Machine and references
Exact model, chase size, first cutting line, sheet direction and Centerline references if any are checked. Gripper margin and tooling reference are not used interchangeably.

MACHINE • MATERIAL • CUTTING DIE COMPATIBILITY
From cutting to creasing, from sheet transport to stripping: we evaluate your cutting die together with the BOBST machine you will use it on and your material.
CUTTING DIE PREPARATION FOR BOBST
"BOBST cutting die" does not define a single dimension or tooling layout. The exact machine model, chase and counterplate system, sheet properties and stations to be used are handled together.
At Özkardeşler, we evaluate the technical drawing with this information, clarifying the scope of cutting, creasing and auxiliary details before the quote. If there is a need for stripping and blanking, we also discuss them as part of the same job.
Exact model, chase size, first cutting line, sheet direction and Centerline references if any are checked. Gripper margin and tooling reference are not used interchangeably.
Cutting rule and creasing specifications are selected together with actual material thickness, grain or flute direction and counterplate system. The folding result is as important as the crease on the flat sheet.
Sheet transport, separation of parts from the cutting die and waste evacuation are considered together. No single recipe fits every job for nick position, rubber profile and layout.
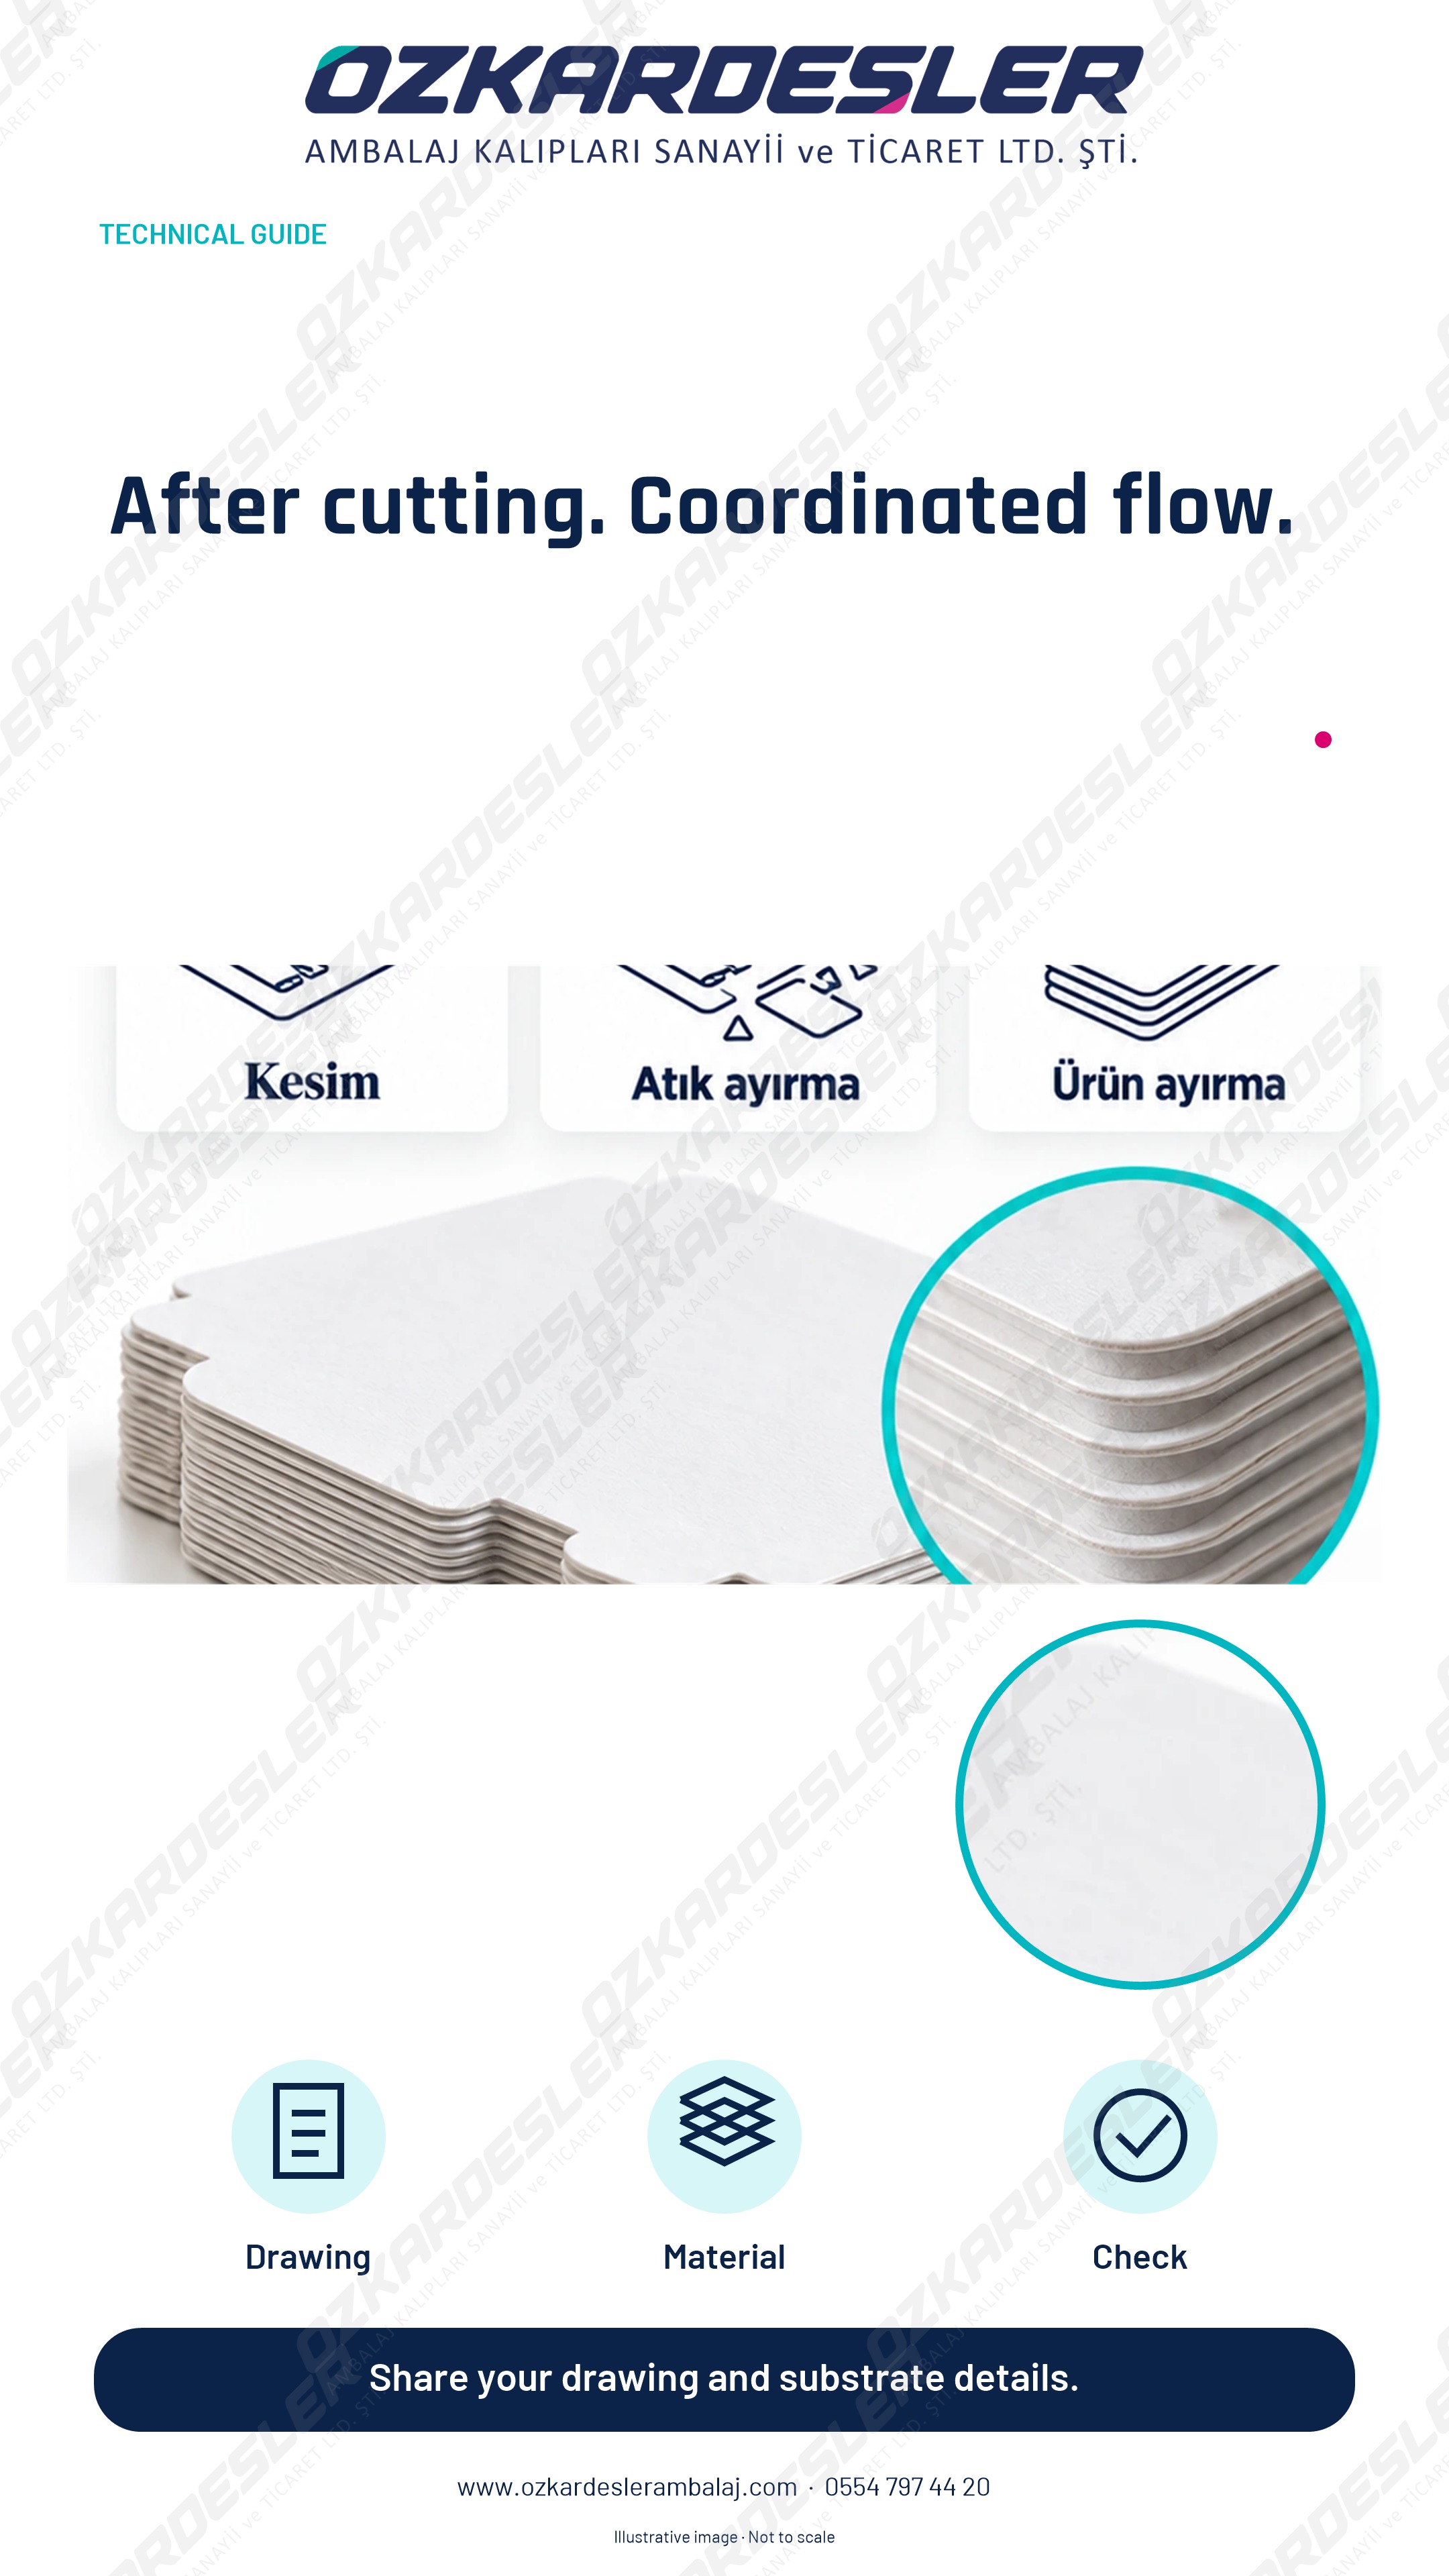
Stripping removes waste; blanking separates products from each other. The stations on your machine and the requested tooling scope are further clarified through the drawing.
ÖZKARDEŞLER PRODUCTION INFRASTRUCTURE
We match the verified equipment in our machinery park with the job drawing and required tooling scope.
02 / PRE-QUOTATION
Attach your drawing if ready. If there is missing information, we can start with dimensions, photographs or sample details.
Open quote form ↗If cutting dies and stripping and blanking tools will be used together, check that all drawings belong to the same product layout and file version. A change in a blank, a small window or a waste connection can also affect the operating layout of other stations.
Instead of just saying "complete set" in the quote, specify which stations the tooling is requested for. If existing dies will be used, share their codes, reference dimensions and latest approved drawings. The difference between waste stripping and blanking helps clarify this scope.
When incomplete cutting, print-to-cut register variation, or irregular waste stripping is observed, mark the feed edge and the problematic blank on the sample. Record whether the defect occurs in the same position on every sheet, on specific blanks, or at variable locations. Examining the cut flat sheet together with the assembled product makes it easier to separate cutting and creasing issues.
Send the records you prepared for the print-to-cut register check list and maintenance or new cutting die evaluation along with your drawing. Let us not determine a definitive cause or standard setting value based on a single trace.
FREQUENTLY ASKED QUESTIONS
No. A single cutting-rule height should not be assumed without verifying the model, chase, and counterplate arrangement. We proceed with the current machine and tooling data.
The compatibility of the chase, references, rule and counter arrangement, and waste stripping equipment must be examined. A similar outer dimension alone does not prove compatibility.
Our current form accepts PDF, DXF, CF2, EVD, PNG, JPG, and WEBP files. There is a maximum limit of 5 files and a total of 10 MB. Receiving the file does not mean technical suitability approval; we evaluate the drawing separately.
LET'S START WITH YOUR DRAWING
Send your drawing, material, and BOBST model information to our team via the quote form.
Submit your project ↗Technical note: Grammage and creasing adjustmentContinue with the checklist matching your topic.